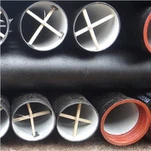
Due to various factors, defects such as air hole, pinhole, slag inclusion, crack, pit and so on often appear in ductile iron castings. The commonly used repair equipment is argon arc welding machine, resistance welding machine, cold welding machine, etc., which has an important impact on the quality, manufacturing cost, production efficiency, labor intensity, environmental pollution and other aspects of ductile castings. As long as the molding and core making processes are well controlled, the quality of the nodular cast slab can be improved.
When lifting the plate of nodular casting, in order to prevent deformation of the plate of nodular casting, four steel wire ropes of the same length shall be used to hang the four lifting holes on the plate of nodular casting at the same time, and the plate of nodular casting shall be stably lifted on the transportation tool. The supporting points of the plate of the ductile casting shall be well padded and leveled. Each supporting point shall be evenly stressed and the whole plate of the ductile casting shall be stable. In order to prevent the overall deformation of the ductile casting plate, the workpiece shall be removed from the ductile casting plate after use to prevent the deformation of the ductile casting plate caused by the workpiece's long-term heavy pressing on the ductile casting plate.
Welding technology will be involved in many processes, including nodular cast iron. The welding processes here are gas welding and manual arc welding, corresponding to different welding wires and treatments. For gas welding, RZCQ type ductile casting welding wire is used, while CJ201 is used as flux and reducing flame is used as flame. In case of processing of castings with complex structure or ductile iron castings, hot welding and slow cooling after welding are also required.
When facing homogeneous weld, the electrode for manual arc welding is EZCQ iron base nodular casting electrode; Before welding, the workpiece needs to be preheated. At the same time, after welding, it needs to be kept warm and slowly cooled. After annealing and welding, cutting can be carried out. Large current and continuous welding process shall be adopted during welding, and the welding current shall also be selected appropriately.
When dissimilar welding seams are used, the welding rods must be changed. The cold welding process must be strictly followed during welding, and the cutting process can only be carried out after cold welding.